High-performance digital hardware and printing terminals engineered for precise color calibration, seamless billing, and industrial management integration.
In the rapidly transforming landscape of global packaging, textiles, and commercial publishing, color fidelity is no longer merely an aesthetic choice—it is a critical currency of international trade. For manufacturers and exporters operating within emerging regional hubs such as the Ngozi market, implementing a robust Color Management System (CMS) bridges the gap between digital pre-press intent and physical production reality. Zhuhai Vector Print Co., Ltd., as a pioneering force in industrial inkjet printing solutions, provides the technological backbone required to achieve absolute Delta-E color consistency across cross-border supply chains.
The Ngozi market represents a dynamic commercial intersection in East Africa, characterized by a surging demand for localized packaging materials, textile branding, and promotional print media. As regional enterprises scale their operations to meet international compliance and consumer expectations, the reliance on advanced printing technology has intensified. Local manufacturers face unique challenges, including substrate variability, climate-induced humidity shifts affecting ink absorption, and the stringent color tolerance demands of multinational brand owners. Integrating a comprehensive Color Management System enables Ngozi-based exporters to calibrate their output locally while seamlessly meeting international export standards.
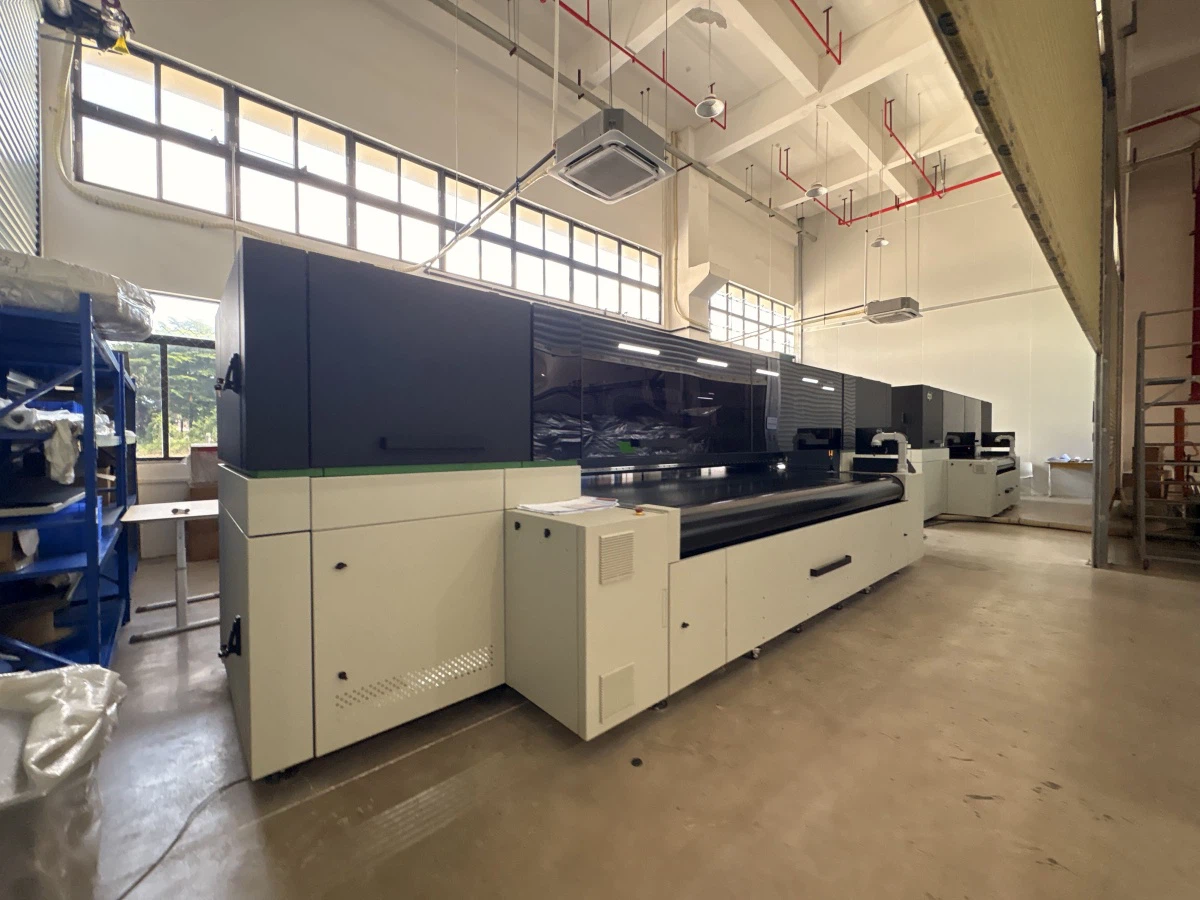
Globally, the printing manufacturing sector is undergoing a profound paradigm shift from analog offset methods to high-speed digital inkjet production. According to recent market research, the global industrial printing market is projected to reach unprecedented valuations, driven by the demand for short-run customization, variable data printing, and sustainable production processes. Color Management Systems act as the central nervous system of modern printing plants, utilizing ICC profiles, spectrophotometric feedback loops, and automated RIP (Raster Image Processor) software to eliminate human error, reduce chemical waste, and ensure repeatable output across multi-site manufacturing facilities.
China remains the undisputed epicenter of industrial machinery manufacturing, offering unmatched supply chain integration, engineering talent pools, and cost-effective production scaling. Zhuhai Vector Print Co., Ltd. capitalizes on this industrial ecosystem by designing and fabricating state-of-the-art Single Pass Inkjet Printing Machines, Multi Pass Digital Inkjet Printers, High-Speed Scanning Inkjet Systems, and Industrial Inkjet Printing Controllers. By combining advanced printhead integration, intelligent ink delivery systems, and rigorous quality control protocols, Chinese manufacturers deliver enterprise-grade reliability at highly competitive price points, empowering global exporters to maximize their Return on Investment (ROI).
Color Management Systems and high-precision digital printing architectures find extensive utility across various vertical sectors within emerging markets like Ngozi:
The future of printing manufacture lies in the convergence of Artificial Intelligence (AI) and closed-loop color control. Emerging trends highlight predictive color maintenance, where machine learning algorithms detect printhead nozzle degradation and automatically adjust ink volume compensation in real-time. Furthermore, cloud-based CMS platforms allow multinational brands to push master color profiles instantly to manufacturing partners worldwide—whether in major global metropolises or regional hubs like Ngozi—guaranteeing absolute uniformity regardless of geographic boundaries.
International corporate buyers and procurement directors evaluating printing manufacturing partners prioritize several key pillars:
Zhuhai Vector Print Co., Ltd. is a technology-driven enterprise specializing in advanced industrial inkjet printing solutions for modern manufacturing. Located in Zhuhai, a key innovation hub in southern China, the company focuses on developing high-performance systems that deliver precision, speed, and reliability across diverse industrial applications.
The company’s core product portfolio includes Single Pass Inkjet Printing Machines, Multi Pass Digital Inkjet Printers, High-Speed Scanning Inkjet Systems, and Industrial Inkjet Printing Controllers. These solutions are engineered to meet the evolving demands of industries such as ceramics, packaging, textiles, and building materials, enabling high-resolution output and consistent production quality.
Zhuhai Vector Print Co., Ltd. operates from a well-equipped production facility and is supported by a skilled team of engineers, R&D specialists, and technical service professionals. By integrating advanced printhead technology, intelligent control systems, and optimized ink delivery solutions, the company ensures stable performance and efficient workflow integration.
Committed to innovation and customer satisfaction, Zhuhai Vector Print continues to invest in research and development while expanding its global presence. The company aims to provide reliable, scalable, and future-ready inkjet printing systems that help manufacturers enhance productivity and stay competitive in a rapidly evolving market.
A Color Management System ensures that digital design files translate accurately into physical printed products regardless of substrate variations. For exporters in Ngozi, it guarantees compliance with international brand color guidelines, reduces expensive print waste, and builds long-term trust with global buyers.
We integrate cutting-edge industrial printhead technology, advanced proprietary RIP software, intelligent closed-loop color calibration, and robust industrial inkjet printing controllers that manage ink viscosity and droplet placement with micron-level accuracy.
Yes. Our R&D and engineering teams specialize in tailoring Single Pass and Multi Pass digital printing systems to meet unique factory specifications, local substrate characteristics, and specific workflow requirements across international markets.
We provide comprehensive global support, including remote diagnostics, professional online installation guidance, operator training modules, and rapid dispatch of replacement parts to ensure maximum operational uptime.
Explore our diverse catalog of high-performance manufacturing, automation, medical, and agricultural hardware solutions designed for global industrial excellence.
 Vector Print