Printing factories are facing tighter margins, volatile paper prices, rising energy bills, and persistent labor shortages. Smithers’ The Future of Global Printing to 2029 identifies packaging, labels, and digital production as important growth areas, but growth alone does not guarantee profitability. A busy pressroom can still lose money through setup waste, idle equipment, overtime, and poorly controlled reprints.
This guide examines how to reduce operational costs in printing factories through practical, measurable actions. The focus is not simply on cutting budgets. It is on improving production decisions, from prepress file checks to ink usage, preventive maintenance, energy monitoring, and finished-goods handling. PRINTING United Alliance industry reports consistently highlight materials, labor, and equipment utilization as major operational concerns for printers. Those pressures appear on the factory floor: a misregistered color run can consume pallets of paper, while a small maintenance delay can disrupt an entire shift.
Energy deserves attention. The U.S. Environmental Protection Agency’s ENERGY STAR program reports that well-managed facilities can often achieve substantial energy savings through monitoring, controls, and operational improvements. However, every factory is different. A recommendation that works for a high-volume web press may fail in a short-run sheet-fed plant. That limitation matters.
The following ten methods connect cost reduction with real production evidence. They cover waste prevention, scheduling, automation, supplier management, and workforce capability. Some results may be modest at first. Measure them honestly. Then improve them.
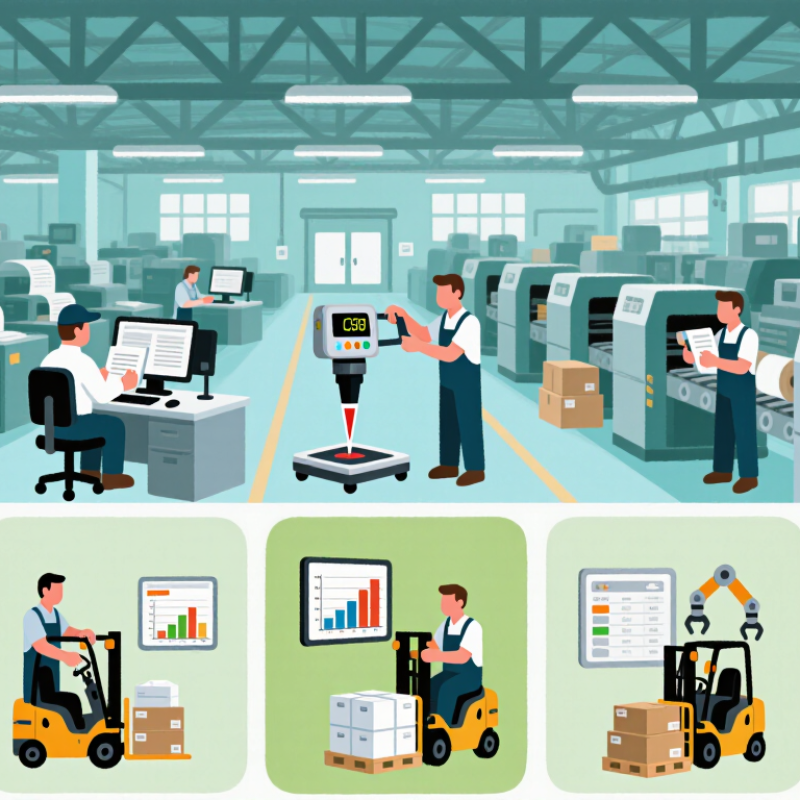
Top 10 Ways to Reduce Costs in Printing Factories?
Materials commonly account for 30–50% of total printing costs. A reliable cost audit must examine more than supplier invoices. Track paper, board, film, ink, plates, coatings, and packaging by job. Review at least twelve weeks of purchasing and production records. Match material received with finished output, waste, returns, and remaining stock. Simple records often expose expensive habits.
During one press-floor review, a 10,000-sheet order showed 8% setup waste. After including reprints, trimming, color approvals, and moisture damage, the real loss reached 13%. Our first estimate was wrong. Measure opening stock, receipts, closing stock, and actual consumption. Compare standard usage with results by machine, shift, and substrate. Small differences become significant across thousands of jobs.
Reduce waste through better sheet layouts, accurate job planning, and controlled purchasing. Do not choose the cheapest material automatically. Check opacity, thickness, drying behavior, surface defects, and runnability through a documented trial. A lower unit price can increase stoppages and rejects. Set reorder points based on demand, not guesswork. Review slow-moving stock monthly. Data quality may remain imperfect, but correcting inconsistent records can reveal savings before any equipment investment.
Materials are typically the largest cost category in commercial printing, accounting for approximately 30–50% of total production costs. Paper, board, ink, coatings, and consumables should be monitored through supplier negotiation, waste reduction, accurate job estimation, and inventory control. The figures shown are representative industry benchmark estimates and may vary by process, product mix, and region.
Makeready waste often hides in small, repeated delays. A press waits while operators adjust color, registration, pressure, and cutting alignment. Sheets accumulate beside the delivery unit. The cost is easy to miss until monthly paper usage is reviewed.
Standardized setups can target 10–20% savings when the process is measured carefully. Record the approved settings for common stocks, ink coverage, plate specifications, and finishing requirements. Keep these records near the machine, not inside an unused office folder. A setup sheet should show the first acceptable proof, actual waste count, adjustment time, and operator notes. Clear photos can also reveal correct guides and roller positions.
Use the same sequence for every comparable job. Stage paper, plates, tools, and approved samples before production starts. Check moisture and paper direction before loading the feeder. Assign one person to confirm color targets and registration during the first run. Small checkpoints prevent expensive guessing.
The target will not fit every job. Unusual substrates, short runs, and urgent changes can disrupt the standard method. That is useful evidence, not failure. Review those exceptions weekly and revise the setup sheet only when production data supports it. Avoid chasing impressive percentages without checking reprints, overtime, and rejected sheets. A cheaper makeready is valuable only when the final saleable output remains consistent.
Raising press OEE toward the 85% world-class benchmark can reduce printing costs without adding another press. OEE measures availability, performance, and quality. Each percentage point should connect to a real production loss.
Start with accurate downtime records. A five-minute stoppage often becomes invisible when operators record only major breakdowns. Track setup delays, material changes, cleaning, plate adjustments, and waiting for approval. During one shift, a simple whiteboard can reveal repeated losses near the first roll change. That detail matters.
Improve setup work with standard checklists and prepared tools. Keep approved job data, inks, plates, and substrates ready before the press stops. Train operators to identify small defects early, such as color drift, registration movement, or uneven drying. Inspecting the first sheets prevents larger waste later. Preventive maintenance also protects speed. Clean sensors, inspect rollers, and check tension systems on a fixed schedule.
Do not chase speed blindly. A faster press can create more rejects. Measure good output against planned production time, not impressive machine speed. Review OEE at each shift meeting, using the same definitions every day. A weak point may be data quality rather than equipment efficiency. That is easy to overlook. The 85% target is useful, but every factory has different products, substrates, and order patterns. Some losses will remain. The better question is whether each loss is understood, measured, and steadily reduced.
Printing factories often lose money through energy waste that is difficult to see. Dryers, compressors, chillers, and ventilation systems may run during idle production hours. An ISO 50001 program creates a structured method for measuring and improving energy performance. Well-managed projects commonly target 5–15% energy savings, although actual results depend on equipment age, production schedules, and staff involvement.
Begin with a practical energy review, not assumptions. Install temporary meters on high-load equipment and compare readings with production output. A press consuming power during setup may reveal more waste than a fully loaded shift. Operators can record temperature, pressure, and startup delays beside each machine. These details connect energy use with downtime, scrap, and maintenance costs.
Small corrections matter. Repair compressed-air leaks, adjust dryer settings, and shut down conveyors during extended pauses. Preventive maintenance also reduces unplanned stoppages caused by blocked filters, worn bearings, or unstable temperatures. However, not every saving survives daily pressure. Workers may bypass controls when targets feel unrealistic. That weakness deserves attention. Training, visible performance boards, and monthly reviews can turn procedures into habits. Managers should verify savings against production volume, seasonal conditions, and product mix. Otherwise, a lower energy bill may simply reflect fewer orders, not better efficiency.
In a printing factory, quality failures rarely begin at the packing table. They often start with small shifts in ink density, paper moisture, plate alignment, or drying temperature. Six Sigma gives managers a disciplined way to measure these shifts and reduce variation. Its familiar benchmark, 3.4 defects per million opportunities, is a target for a highly controlled process, not a promise for every job. A practical team first defines a defect clearly. Is a faint streak one defect, or ten defects across ten labels? That decision changes the data.
Operators can record color readings, registration errors, jams, and rejected sheets during each press run. A quality engineer can map the process, investigate root causes, and test changes in small batches. For example, stabilizing paper humidity may reduce curl before trimming. Automatic cameras can identify missing text or uneven coverage in real time. Statistical dashboards can also reveal recurring patterns. Automation saves inspection labor, but it cannot repair poor sampling or unclear specifications. Some teams chase impressive numbers while ignoring setup waste. That is an uncomfortable lesson. Six Sigma works only when measurements reflect customer requirements and operators trust the records.
Tips: Define defects before collecting data. Track every production opportunity, not only rejected sheets. Calibrate sensors regularly. Review false alarms with experienced operators. Start with one press line, then expand after the results remain stable. Allow room for judgment; machines can miss unusual defects.
Practical cost-reduction framework using measurable production, quality, maintenance, energy, and inventory controls
| No. | Cost-Reduction Method | Printing-Factory Application | Measurable KPI | Reference Target or Fact | Savings Calculation | Main Cost Driver Reduced |
|---|---|---|---|---|---|---|
| 1 | Automate Quality Control with Six Sigma | Use inline cameras, color sensors, registration monitoring, barcode verification, and automatic defect classification during printing and finishing. | Defects per million opportunities (DPMO); first-pass yield; customer complaint rate. | 3.4 DPMO is the commonly cited Six Sigma benchmark under the standard 1.5-sigma shift convention. | Avoided cost = rejected units × unit conversion cost + rework hours × labor rate + return and complaint cost. | Waste, rework, returns, inspection labor, and material consumption. |
| 2 | Reduce Make-Ready and Changeover Time | Standardize plate, die, ink, substrate, and tooling preparation; move external setup activities away from machine downtime. | Changeover minutes; setup waste sheets; jobs completed per shift. | Track internal and external setup separately using SMED principles; the objective is continuous reduction of internal setup time. | Recovered capacity = minutes saved per changeover × changeovers × contribution margin per machine minute. | Machine downtime, overtime, setup materials, and lost production capacity. |
| 3 | Improve Overall Equipment Effectiveness (OEE) | Separate availability, performance, and quality losses for presses, digital printers, cutters, folders, laminators, and binders. | OEE = availability × performance × quality. | Use the standard three-factor OEE calculation; set an internal baseline before assigning improvement targets. | Capacity recovered = rated output × increase in OEE × available production time. | Idle time, slow running, minor stops, and quality losses. |
| 4 | Adopt Preventive and Predictive Maintenance | Schedule maintenance from operating hours and condition data; monitor vibration, temperature, pressure, and bearing status where appropriate. | Unplanned downtime hours; mean time between failures (MTBF); mean time to repair (MTTR). | MTBF measures average operating time between failures; MTTR measures average repair duration. Both should be trended by asset. | Avoided downtime cost = prevented failure hours × contribution margin per machine hour. | Emergency repairs, spare parts, overtime, and unplanned downtime. |
| 5 | Control Substrate and Material Waste | Use automated web-break detection, optimized imposition, accurate job nesting, roll-length tracking, and closed-loop waste reporting. | Waste percentage = waste material ÷ total material issued × 100. | Measure setup waste, process waste, trim waste, spoilage, and overruns as separate categories. | Material savings = reduction in waste quantity × purchased material cost per unit. | Paper, board, film, labels, packaging stock, and disposal fees. |
| 6 | Optimize Ink, Coating, and Chemical Consumption | Use calibrated dispensing, viscosity or pH monitoring where applicable, standardized recipes, and controlled wash-up procedures. | Ink or coating usage per 1,000 sellable impressions; wash-up volume per changeover. | Compare actual usage with the approved job estimate and investigate variance by press, substrate, and operator. | Consumable savings = baseline usage − actual usage, multiplied by the current purchase price. | Ink, varnish, coating, solvents, cleaning agents, and hazardous-waste handling. |
| 7 | Reduce Energy Consumption | Submeter high-load equipment, eliminate compressed-air leaks, optimize drying and curing settings, and shut down idle equipment safely. | kWh per 1,000 sellable impressions; peak demand; compressed-air loss rate. | Energy intensity should be normalized by sellable output rather than machine runtime alone. | Energy savings = reduced kWh × electricity tariff + reduced peak demand × demand charge. | Electricity, gas, compressed air, drying, curing, and HVAC costs. |
| 8 | Improve Production Scheduling and Workflow | Sequence jobs by substrate, ink or coating requirements, finishing route, delivery date, and setup similarity. | On-time delivery; schedule adherence; work-in-process days; queue time. | Use finite-capacity scheduling so planned work does not exceed available machine, labor, or finishing capacity. | Cost avoided = overtime hours + expedited freight + idle labor + late-delivery penalties. | Overtime, expediting, idle labor, excess WIP, and late-order costs. |
| 9 | Optimize Inventory and Purchasing | Classify stock by usage and criticality; set reorder points from demand, lead time, and safety-stock requirements. | Inventory turns; stockout frequency; obsolete inventory value; supplier on-time delivery. | Reorder point = expected demand during lead time + safety stock. | Working-capital release = inventory reduction × material carrying-cost rate. | Storage, financing, obsolescence, rush purchasing, and stockout disruption. |
| 10 | Automate Data Capture and Standard Work | Connect job tickets, machine counters, inspection results, maintenance records, and material usage to a centralized production dashboard. | Manual data-entry hours; reporting delay; traceability completeness; corrective-action closure time. | Use controlled work instructions, versioned process parameters, and electronic records for traceability. | Administrative savings = eliminated data-entry hours × labor rate; quality savings come from faster root-cause response. | Administrative labor, reporting errors, delayed decisions, and recurring process failures. |
Track paper, board, film, ink, plates, coatings, and packaging. Review supplier invoices and job-level consumption. Material costs may reach 30–50% of total printing costs.
Review at least twelve weeks of records. Compare opening stock, receipts, closing stock, and actual consumption. Short reviews can hide seasonal waste.
Match materials received with finished output, returns, reprints, and remaining stock. Include setup waste, trimming, color approvals, and moisture damage. An 8% setup loss can become 13% overall.
No. Test opacity, thickness, drying behavior, surface quality, and runnability. A cheaper sheet may cause jams, stoppages, or rejected prints. The lower price may mislead.
Set reorder points according to demand and production records. Review slow-moving stock every month. Correct inconsistent records before buying new equipment.
Define defects before collecting data. A faint streak might count as one defect or several affected labels. That choice changes the results.
Cameras can detect missing text, uneven coverage, and registration errors during production. Sensors should be calibrated regularly. Machines still miss unusual defects.
Begin with one press line and test small changes. Track color readings, jams, rejected sheets, and process conditions. Review false alarms with experienced operators. The records may remain imperfect.
Reducing costs in a printing factory begins with a detailed audit of the cost base. Materials can account for 30–50% of total print costs, so reviewing paper, ink, plates, and purchasing practices is essential. Factories can also reduce makeready waste by standardizing press setups, improving job scheduling, and training operators, with a realistic target of 10–20% savings. Increasing press effectiveness is another major opportunity: monitoring uptime, speed, and quality can help factories move toward the 85% world-class OEE benchmark.
A complete plan for how to reduce operational costs in printing factories should also address energy use, unplanned downtime, and quality losses. Energy monitoring and structured improvement programs may achieve 5–15% savings, while preventive maintenance keeps equipment productive. Automated inspection and data-based quality control can reduce defects and rework, supporting a Six Sigma goal of 3.4 defects per million opportunities. Together, these measures create a more efficient, consistent, and financially sustainable printing operation.
Vector Print