Printhead performance determines more than image sharpness. It influences production speed, ink usage, maintenance costs, and customer confidence. A weak nozzle can create a visible line across a label. A small temperature change can alter droplet size. These details matter.
When asking how to improve printhead performance, operators should look beyond the printhead itself. Ink viscosity, waveform settings, substrate texture, humidity, firing frequency, and cleaning routines all interact. A practical evaluation begins with evidence: inspect nozzle test patterns, record operating temperatures, measure downtime, and compare results across shifts. This approach supports reliable decisions instead of guesswork.
Doug Edwards, a former Xaar chief executive and experienced digital-printing specialist, has described the printhead as “the heart of the digital printing process.” That observation remains useful. However, the heart does not work alone. Poor ink filtration or an incorrect waveform can undermine an otherwise advanced printhead. Maintenance is not glamorous. It is essential.
The following guide presents ten practical ways to improve printhead performance. It covers nozzle cleaning, ink conditioning, waveform adjustment, environmental control, alignment, and preventive inspection. Each method connects a technical action with a measurable outcome. Some recommendations may require testing rather than immediate adoption. Real machines behave differently. Even experienced teams can overlook a simple cause, such as dried ink near the capping station. Careful operators keep questioning their assumptions. That habit often protects print quality better than expensive upgrades.
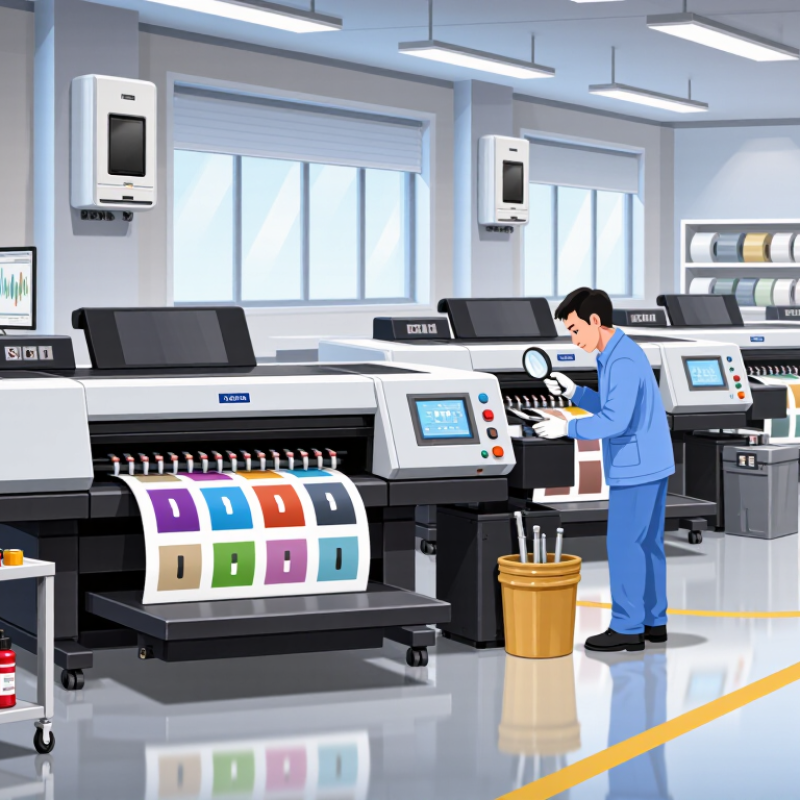
Printhead performance should begin with measurable targets, not vague claims about “high quality.” A practical baseline is 600–1,200 dpi, 1–30 pL drop volume, and stable jetting speed. Higher resolution can sharpen small text, but it may reduce throughput and increase nozzle sensitivity. Smaller drops improve tonal control. They also demand cleaner ink and tighter humidity control. Industry analysis from Smithers, The Future of Inkjet Printing to 2029, identifies resolution, droplet control, and firing frequency as key production variables. In many industrial systems, drop velocity reaches approximately 5–10 m/s, with firing frequencies measured in tens of kilohertz. Measure these values on the substrate, not only in the specification sheet.
Tips: Print a nozzle-check pattern before each shift. Record missing jets, satellite drops, waveform settings, temperature, and humidity. ISO/IEC 24790:2017 supports objective print-quality evaluation, including uniformity and text reproduction. A simple log often reveals problems faster than visual inspection.
In real testing, a clean printhead can still produce uneven density. Paper absorption, ink temperature, and carriage vibration may be responsible. I once treated speed as the main productivity measure; that was incomplete. A 1,200 dpi setting is useless when alignment drifts across a long run. Compare actual dot placement, drop consistency, and usable speed under identical conditions. Allow a small tolerance, because laboratory perfection rarely survives production. Recheck the target after maintenance, ink changes, and seasonal humidity shifts.
| No. | Performance Improvement Area | Recommended Practice | Primary Metric | Reference Target or Operating Range | How to Verify |
|---|---|---|---|---|---|
| 1 | Match Resolution to the Application | Select a native or effective addressable resolution that supports the required detail without creating unnecessary data load or excessive firing frequency. |
Resolution: 600–1,200 DPI Line-pair or edge-detail reproduction |
600 DPI for general graphics 1,200 DPI for fine text, codes, and detail |
Print a calibrated resolution chart and inspect fine lines, small text, and edge definition at production speed. |
| 2 | Control Drop Volume | Use the smallest stable drop volume that provides adequate optical density, coverage, and adhesion for the substrate. |
Drop volume: 1–30 pL Dot diameter and optical density |
1–5 pL for fine detail 10–30 pL for solid coverage |
Measure drop mass or volume using validated equipment, then compare printed dot gain and density against the process standard. |
| 3 | Optimize Jetting Speed | Tune waveform and fluid temperature so drops leave the nozzle cleanly, with sufficient velocity and minimal satellite formation. |
Jetting speed: typically 5–10 m/s Drop velocity variation |
Stable velocity within ±5% Low satellite-drop frequency |
Use high-speed imaging or an in-line drop-monitoring system to measure velocity, trajectory, ligament length, and satellites. |
| 4 | Maintain Fluid Viscosity | Keep ink or coating viscosity within the printhead supplier’s qualified process window and compensate for temperature-related changes. |
Viscosity at controlled temperature Temperature stability |
Use the validated fluid window Temperature variation typically ≤ ±2°C |
Measure viscosity with a calibrated viscometer at the actual operating temperature before and during production. |
| 5 | Filter and Degas the Fluid | Remove particles and dissolved air before the fluid reaches the nozzle plate; use filtration compatible with the fluid chemistry. |
Particle count Dissolved or entrained air level |
Filter rating based on nozzle size No visible bubbles in the fluid path |
Record filter condition, inspect the fluid path, and monitor missing-nozzle events after fluid changes or maintenance. |
| 6 | Keep Nozzles Clean | Apply scheduled wiping, capping, and approved purge routines to prevent dried fluid, dust, and residue from disturbing drop direction. |
Nozzle-out rate Drop-direction error |
At least 99% active nozzles Consistent drop trajectory |
Run a nozzle check before production and compare the printed test pattern with the baseline after each cleaning cycle. |
| 7 | Tune the Drive Waveform | Adjust voltage, pulse width, rise time, and dwell timing together rather than changing one parameter without checking the complete waveform. |
Drop volume and velocity Satellite count |
Stable primary drop Minimal satellites and nozzle-to-nozzle variation |
Test one controlled variable at a time and document the waveform, fluid condition, drop volume, speed, and image quality. |
| 8 | Improve Head-to-Substrate Alignment | Set the printhead height, angle, and lateral alignment to reduce flight distance, skew, and positional error across the print swath. |
Placement error Head-to-substrate gap |
Use the approved mechanical gap Placement error within the application tolerance |
Print registration marks in both directions and measure deviation at the beginning, center, and end of the print area. |
| 9 | Synchronize Motion and Firing | Coordinate encoder feedback, carriage or web speed, firing frequency, and image data timing to avoid banding and spacing errors. |
Effective firing frequency Registration and banding level |
Firing frequency matched to speed and DPI Repeatable registration across the print |
Increase production speed in controlled steps and inspect periodic banding, line spacing, registration marks, and encoder logs. |
| 10 | Track Reliability and Preventive Maintenance | Establish a trend log for nozzle health, purge cycles, fluid temperature, viscosity, drop performance, and print defects. |
Mean time between cleaning Printhead availability and defect rate |
Stable results over the production shift Cleaning intervals based on measured degradation |
Review daily trend charts and trigger maintenance when nozzle-out rate, density, registration, or drop placement exceeds the control limit. |
Many systems work near 8–12 cP. However, this range is not universal. Verify the equipment specification before changing ink chemistry.
Viscosity can change significantly between 25°C and 35°C. Lower resistance may alter droplet formation and firing consistency.
A practical range is about 28–35 mN/m. The suitable value depends on the nozzle plate and waveform settings.
A 2 mN/m shift changed nozzle-plate wetting during one trial. Drop placement then became inconsistent. That result was surprising.
Measure viscosity, surface tension, density, and particle size. Record the results before loading the ink.
Yes. Evaporation can increase solids over time. The ink may then produce satellites, missing nozzles, or edge curl.
Keep it within ±1°C. During critical color runs, a tighter target near ±0.5°C is useful.
Place sensors near the printhead, not only inside the cabinet. Compare readings with ink temperature, room temperature, and print speed.
Check temperature control, filtration, degassing, ink storage, and waveform settings together. One stable reading proves very little.
Use trend charts, alarm limits, and verified sensors before adjusting firing parameters. I once blamed software; a loose sensor mount was responsible.
Improving printhead performance begins with defining measurable targets, such as resolution between 600 and 1,200 DPI, drop volumes from 1 to 30 pL, and stable jetting speed. The next step is matching the ink chemistry to the printhead’s approved operating window. Maintaining viscosity around 8–12 cP and consistent surface tension can support reliable droplet formation while reducing misfires and uneven coverage.
To understand how to improve printhead performance in practice, operating conditions must also be carefully controlled. Keep the printhead temperature within ±1°C, then tune waveforms and firing rates across the 20–50 kHz range to achieve clean, consistent drops. Improvements should be verified using nozzle-out counts, drop velocity measurements, and satellite-rate analysis. Together, these checks help identify instability early, optimize image quality, and extend dependable operation.
 Vector Print